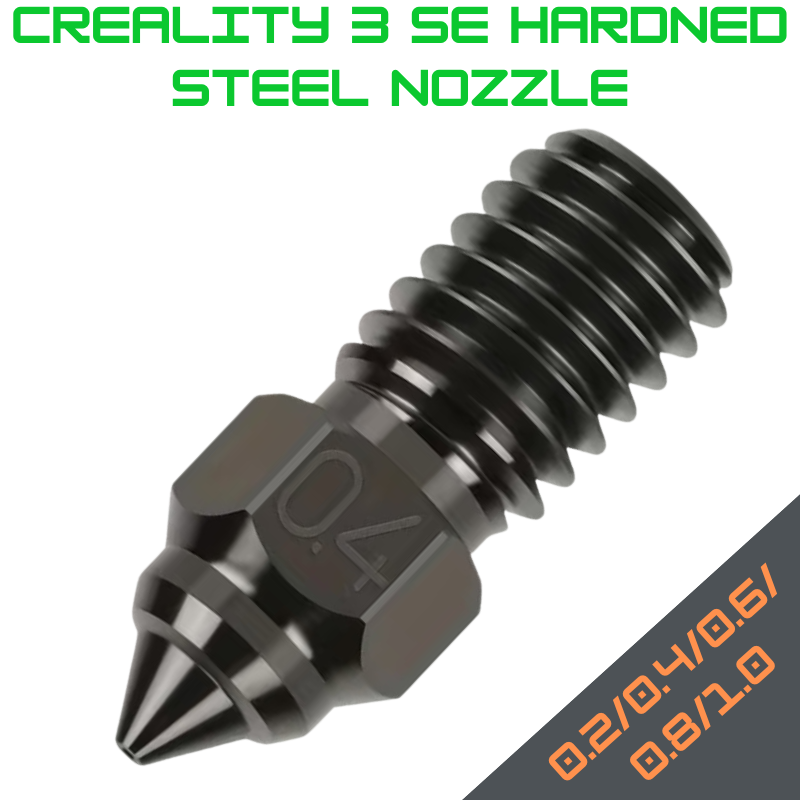
Only suitable for 3D Printer hotend and Spider 1.0 hotend kit.
The Nozzle is a precision-machined extrusion tip designed for Ender 5 S1/Ender 7/Ender 3 V3 SE printers. Made from high‑quality Hardened Steel, this nozzle provides excellent thermal transfer for consistent melt and smooth flow with ABS, PETG, ASA, PP, PA and other standard thermoplastics. Available in a range of orifice sizes (commonly 0.2 mm, 0.4 mm, 0.6 mm, 0.8 mm, 1.0), the nozzle lets you trade off resolution versus print speed and material flow to suit every project — from fine detailed models to rapid prototyping and functional parts.
Key features
- Precision-machined for superior thermal conductivity and smooth filament flow
- Compatible with Ender 5 S1/Ender 7/Ender 3 V3 SE printers.
- Multiple nozzle sizes available: 0.2 / 0.4 / 0.6 / 0.8 / 1.0 mm
- Standard M6 thread (verify before ordering) and typical nozzle length for these printers.
- Ideal for common filaments: PLA, ABS, PETG, TPU, PP, PA (soft filaments may require careful retraction tuning)
Typical technical specifications
- Material: Hardened Steel
- Thread: M6
- Orifice diameters: see SKU (0.2–0.8 mm typical)
- Overall length: ~16.8 mm
- Thread Length: ~9.2 mm
- Recommended nozzle temperature range: 180–360 °C depending on filament type
- Compatibility: Hotends and many clone extruders (verify thread/length compatibility before purchase)
Compatibility & fitment notes
- Confirm your printer uses this style of nozzle with M6 threading. Some all-metal hotends or proprietary systems use different thread pitches or lengths.
- If your hotend has an integrated heat-break/nozzle assembly with nonstandard dimensions, compare overall length and thread depth to avoid gap or over-tightening.
- Use a torque-limited wrench or two wrenches (one on the heater block, one on the nozzle) to avoid twisting the heat-break when installing.
Usage recommendations
- For fine detail prints, use 0.2 mm nozzles (slower, higher resolution).
- For general-purpose printing, 0.4 mm gives the best balance of speed and detail.
- For faster or stronger prints and thicker layers, use 0.6–0.8 mm nozzles.
- Increase extrusion multiplier / flow and layer height proportionally when using larger nozzle diameters.
Cleaning & maintenance
- Engineered for abrasive filaments (carbon fiber, metal‑filled, glow‑in‑the‑dark) which will wear the orifice on standard nozzles.
- Regularly clear partial clogs with cold pulls (nylon/acetone-assisted for ABS) or soak in appropriate solvent if necessary.
- Heat nozzle to printing temp and use a fine needle to remove debris carefully. Do not use excessive force.
Safety & handling
- Always heat the nozzle before attempting removal or cleaning to avoid stripping threads and to make filament removal easier.
- Use heat-resistant gloves and tools when handling the hotend.
- Do not overtighten — tighten firmly at operating temperature then cool to seat threads.
No customer reviews for the moment.